
Aerospace Precision Machining Parts: Materials, Documentation and Tolerance Expectations
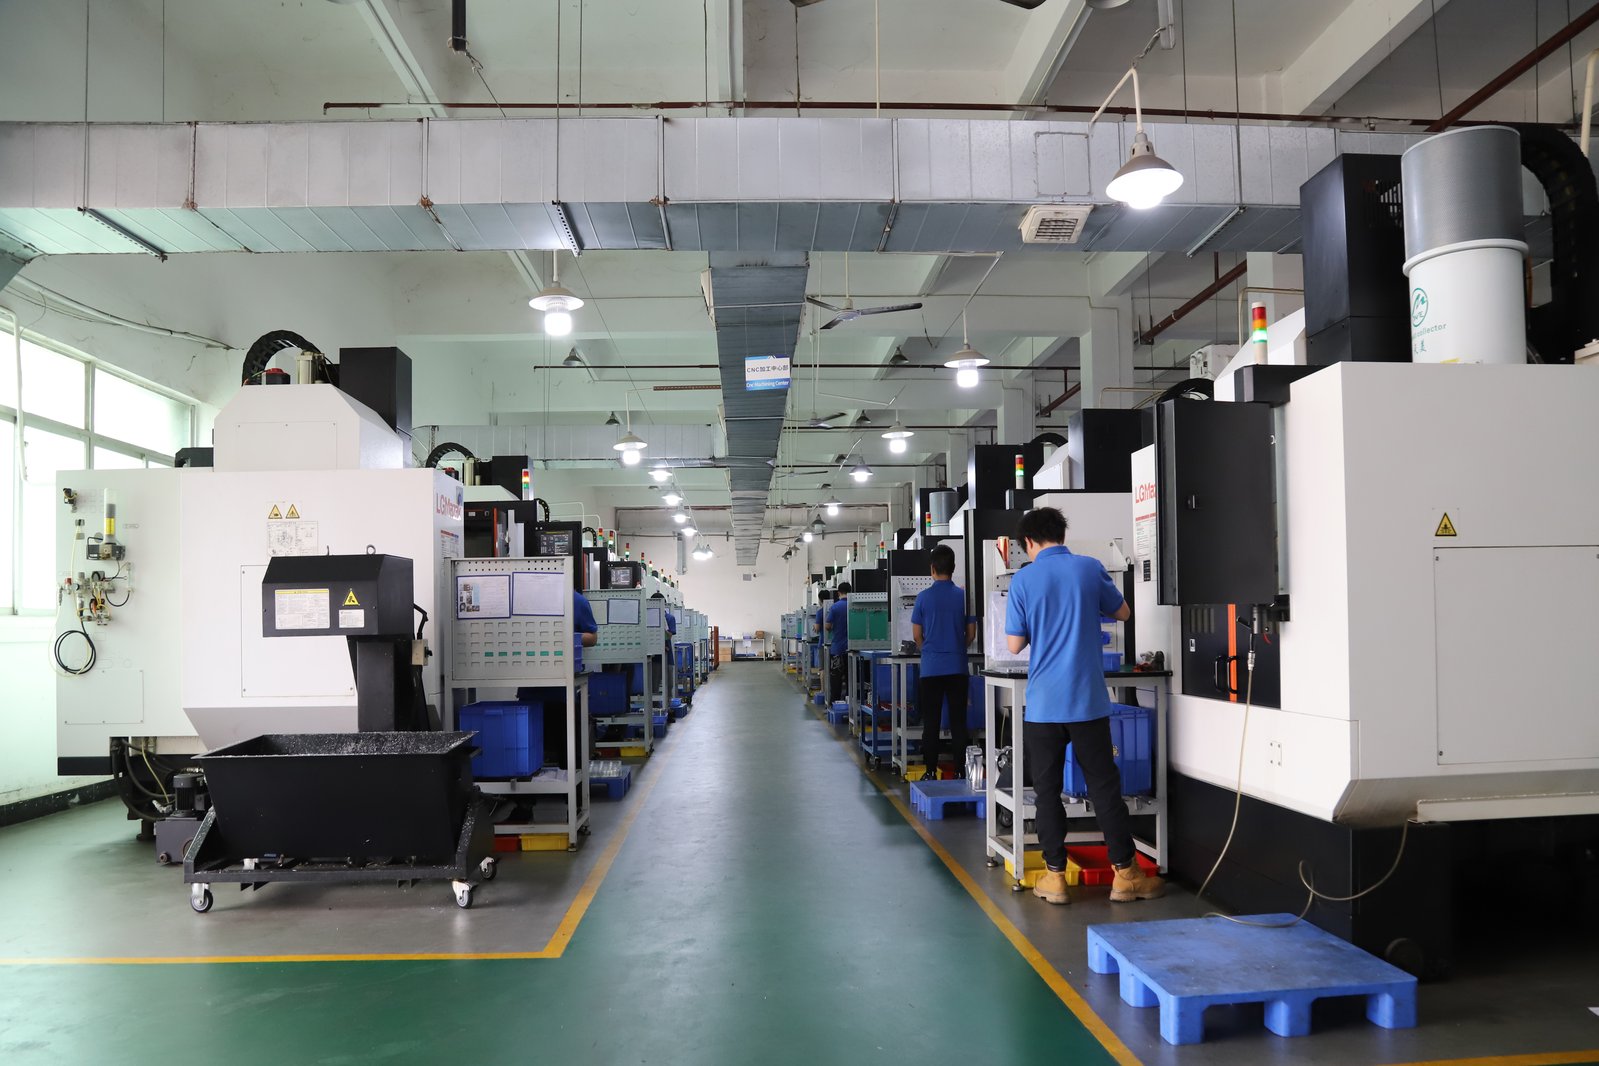
Aerospace precision machining parts carry a heavier expectation than ordinary precision parts, and the difference is not the tolerance — it is the company the material, the documentation, and the measurement evidence have to keep. The buyer who treats an aerospace part like any other machined part discovers the gap at first article; the buyer who sets the expectations up front gets parts whose paper trail matches their function. This guide is the buyer's reference for aerospace precision machining parts: which materials earn a place in an aerospace specification and how their states are verified, what the documentation set has to prove beyond a certificate, which tolerance expectations survive contact with a machined part, and how to write the RFQ so the parts, the records, and the drawing agree.
Why does an aerospace precision part change the material question?
The material question on an aerospace part is not "which alloy is available" but "which material state the design depends on." Aerospace loads punish ambiguity: a bracket assumed to be high-strength 7075-T6 behaves differently if it arrives as a softer temper, and a fitting that must survive corrosion in a 316 or 17-4PH condition has a service life tied to that exact grade and heat treatment. The drawing has to name the alloy, the temper, and the condition, and the shop has to prove it received and ran that state, because a substituted alloy passes every dimension and fails in service, and on an aerospace part the failure is not a warranty claim, it is a grounded aircraft.
On the floor behind this site the material range runs from aluminum through stainless, carbon and alloy steel, brass, copper, titanium, and engineering plastics, with titanium specifically named for aerospace work — the same material map the parts page lays out for buyers, and every incoming lot is verified against its material certificate before cutting, so the grade you specify is the grade that runs. The buyer-side discipline is the same: name the alloy with its condition on the drawing, ask how incoming material is verified, and require the material certificate to travel with the lot. An aerospace material file that ends at a mill certificate is only half a file; the verification record that ties the certificate to the lot that was actually cut is the other half.
Which aerospace alloys are realistic to specify, and where does each belong?
The practical aerospace set is small and well understood. Aluminum 6061-T6 covers structural brackets and housings where strength, corrosion with anodizing, and low cost are enough; 7075-T6 buys higher strength for load-carrying parts at a higher material price and a more demanding cut. Stainless grades like 304, 316, and 17-4PH cover corrosion-critical and high-strength fittings, with 17-4PH earning its place where strength and corrosion meet. Titanium — the Ti-6Al-4V grade — covers the highest-strength, highest-value structural work where weight is the driver, and it costs more in tool wear and slower feeds than any aluminum or steel part. Engineering plastics such as PEEK appear where insulation, weight, or chemical resistance outweighs metal.
The realistic expectation is not that every aerospace part is titanium — it is that each material earns its place on a specific property, and the machining route follows the material. Aluminum cuts fast; stainless needs controlled feeds to avoid work-hardening; titanium forces slower cuts and sharper tools; and each of those routes shows up in the quote and the schedule. When the drawing names the alloy and the property it serves, the quote prices the real route, and the supplier can flag the geometry that fights the material before the first article rather than after it.
What does documentation mean on an aerospace precision part beyond the certificate?
Aerospace documentation is the evidence that the part is what the drawing says it is, and it runs deeper than a quality certificate. The documentation set should tie four things together: the material, with its certificate and the verification record for the incoming lot; the dimensions, with the CMM report that measured the critical features against the drawing; the process, with the record of what was run and by whom; and the acceptance, with the first-article inspection that gates the run. Each document names a number, a machine, and a record, and together they let a reviewer reconstruct the part's history without trusting a memory.
The reason the paper trail matters on aerospace work is traceability: when something goes wrong, the question is not "what did we intend" but "what did we actually ship, and from which lot." On this floor parts trace back through the process to their raw-material lot, so a non-conformance isolates the exact batch instead of stopping the whole program. The buyer should expect the same: ask what documents ship with the parts, what each one proves, and whether the traceability record links the finished part to its incoming material. A documentation set that answers those questions is a file; one that stops at a certificate is a folder with a logo in it.
Which tolerance expectations survive contact with a machined aerospace part?
Set the tolerance expectations the way the process can actually meet them. Milling and turning hold ±0.003 mm on critical features, and precision grinding reaches ±0.002 mm for sealing and seating surfaces, with process capability tracked at Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window., and on an aerospace part the discipline is to spend that precision only where the function lives. A bearing seat, a locating bore, a sealing face, and a hole pattern that carries fasteners earn tight call-outs; a cosmetic web or a clearance hole does not, and over-tolerancing it raises cost and inspection time without adding safety. Reserve the fine bands for the features that assemble or seal, and let the general block carry everything else, exactly as the drawing discipline on this site recommends for every precision part.
The other expectation that survives is the interaction between tolerance, material, and measurement. A tight feature in titanium behaves differently under cutting than the same feature in aluminum, and a ±0.003 mm call-out is only as real as the instrument that verifies it — on this floor critical dimensions are confirmed on CMMs, as the quality page describes, because a tolerance no instrument can prove is a hope, and on an aerospace part hopes are not airworthy. State the tolerance per feature with the instrument that will measure it, and the expectation becomes checkable: the drawing says what is tight, the CMM report proves it is tight, and the Cpk shows the process can stay tight across a run.
How does the prototype-to-production path work for aerospace precision parts?
Aerospace parts rarely jump straight to volume; they move through prototype, first article, and a qualification batch, and each stage carries its own evidence. The prototype proves the geometry and the process route; the first-article inspection measures every critical feature against the drawing and becomes the record the production run is measured against; the early batch proves the process stays in control at a small scale before volume is committed. On this floor a one-piece minimum lets that path start at a single part, with the first article carrying the full measurement record at a cost you can absorb.
The buyer's job is to keep the evidence moving with the part through each stage. The prototype report, the first-article record, and the production SPC data should form one continuous file rather than three unrelated documents, because the first article is only useful if the production run is measured against it. When the same shop runs prototype and production on the same machines with the same measurement bench, the path is continuous — the record you build on the first part carries straight into the run, and the aerospace expectation of traceability is met without re-qualifying the supplier at every step. Ask the supplier to name the records at each stage before you commit, so the documentation you will need at qualification is specified on the order rather than negotiated after the parts are made, that is the difference between an aerospace part with a file and one with an argument.
What should an aerospace precision RFQ state to get comparable quotes?
An aerospace RFQ earns comparable quotes when it states the expectations the drawing cannot carry alone. Name the material with its grade, temper, and condition, and state how the incoming lot will be verified. State the tolerance per critical feature with the measurement method, so that every supplier prices the same CMM-confirmed band. Name the documentation set that must ship with the parts — material certificate, verification record, CMM report, first-article inspection — so the evidence is a condition of the order, not a later request. And name the acceptance criteria, so "delivered" means the same thing to every supplier.
Then grade the quotes on the evidence they include, not on the headline price. A quote that prices the verification and the documentation is pricing the aerospace part; a quote that leaves them out has quoted a cheaper part that does not meet the drawing's full expectation. Because incoming material is verified against its certificate and critical dimensions are confirmed on CMMs before shipping on this floor, the RFQ you write and the parts you receive are governed by the same standard, and the comparison table fills itself once every supplier is quoting the same material, the same tolerance, and the same paperwork.
Frequently Asked Questions
Which materials are realistic for aerospace precision machining parts?
Aluminum 6061-T6 and 7075-T6 for structural parts, stainless 304, 316, and 17-4PH for corrosion-critical fittings, Ti-6Al-4V for high-strength lightweight work, and engineering plastics such as PEEK where they fit the function. The grade, temper, and condition belong on the drawing, not left to the supplier.
Why does documentation matter more on aerospace parts?
Because traceability is the point: when something goes wrong, the question is what was shipped and from which lot. The documentation set should tie the material certificate, the verification record, the CMM report, and the first-article inspection to the finished part, so a reviewer can reconstruct its history.
What tolerance can aerospace precision machining parts hold?
Milling and turning hold ±0.003 mm and precision grinding reaches ±0.002 mm, verified on CMMs with process capability at Ppk ≥ 1.67 initial. The discipline is to spend the precision where the function lives and leave clearance and cosmetic features on the general block.
Is every aerospace part made of titanium?
No. Titanium earns its place where weight and strength are the drivers and the budget allows the slower cut. Most aerospace structural parts are aluminum or stainless; the material should follow the property the part needs, not the prestige of the name.
How is a titanium or stainless grade verified against substitution?
By the incoming material check. On this floor every lot is verified against its material certificate before cutting, and the certificate and verification record ship with the parts. A substituted alloy passes every dimension and fails in service, so the material check belongs in the order, not at the failure.
Can aerospace parts start at a low quantity?
Yes. A one-piece minimum lets the path start with a single prototype and a first-article inspection that carries the full measurement record, then scale through a qualification batch to volume — with the evidence moving continuously through each stage.
What should an aerospace precision RFQ include to get comparable quotes?
The material with grade and condition and its verification method, the tolerance per critical feature with the measurement method, the documentation set that ships with the parts, and the acceptance criteria. Grade the quotes on the evidence they include, not on the headline price.
Working on an aerospace precision machining part and need the evidence to match?
Email the STEP or IGES model with your toleranced 2D drawing to [email protected] or call +86 13126536955. You will get the design-for-manufacturability review, the material states we can verify, and the CMM-based documentation set that ships with the parts.